Why Specification-Grade PDV Salt Dictates Industrial Process Reliability
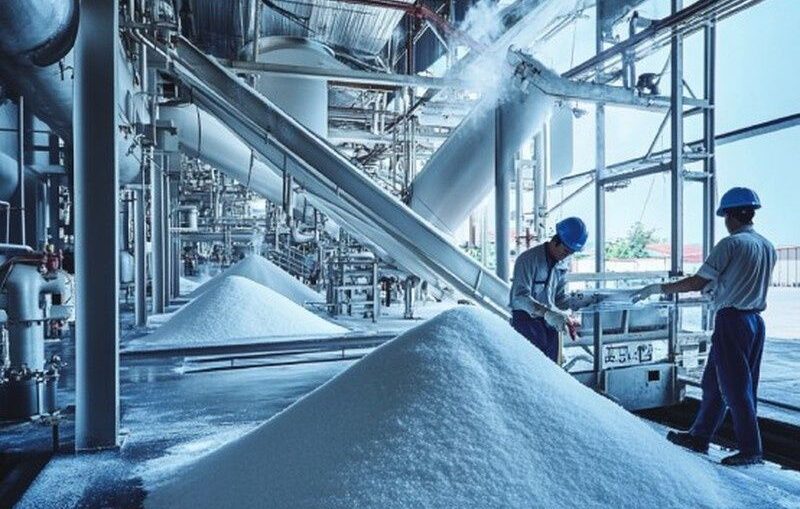
Pure dried vacuum salt, commonly abbreviated as PDV salt, is a controlled raw material rather than a commodity purchased solely by weight. In high-volume water treatment, chemical processing, and regeneration systems, sodium chloride is dissolved, transferred, dosed, and repeatedly exposed to pumps, valves, injectors, saturators, and ion-exchange resin beds. Small variations in moisture, particle size, insoluble matter, or chemical purity can therefore become recurring mechanical and process problems.
The difference between generic commercial salt and certified industrial-grade sodium chloride is especially important when equipment operates automatically. Trace insolubles can accumulate as sludge, while excess moisture promotes clumping, bridging, and inconsistent feeder output. A specification-led approach, based on documented compliance with the applicable standards and supported by lot-level certificates of analysis, gives operations teams a defensible basis for protecting automated batching equipment and extending resin service life. The right grade is not simply the salt with the lowest purchase price; it is the material that delivers predictable dissolution and stable regeneration under the facility’s actual operating conditions.
Regulatory Benchmarks and Chemical Profiles Under BS EN 973 and BS 998
BS EN 973 Class A is widely used as a benchmark for salt intended for regeneration of ion exchangers used in water treatment. BS 998 has historically provided a British specification for salt, including requirements relevant to purity and contaminants. The precise purchasing requirement should always be confirmed against the current contract, application, and applicable edition of the standard, because a product description such as “food grade” does not automatically establish suitability for every industrial regeneration process.
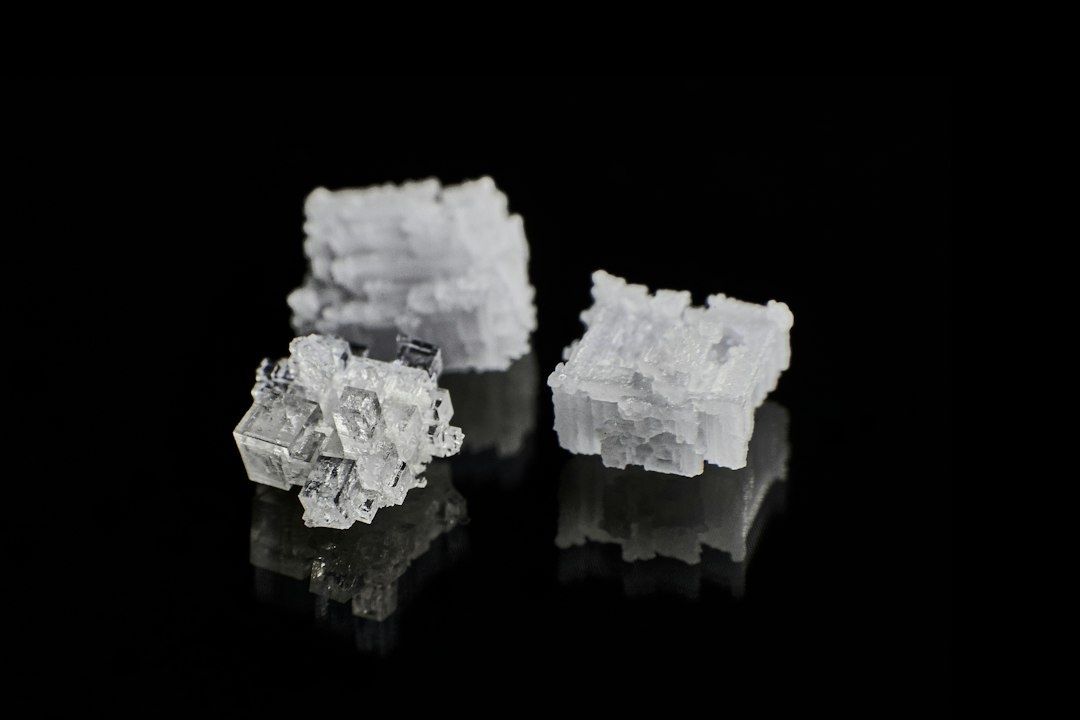
For engineering purposes, the central distinction is between a general commercial product and a material with a defined chemical profile. Under the standard BS EN 973 Grade A, the normative minimum requirement is 99.4 percent sodium chloride calculated on a dry basis (compared to 98.5 percent for Grade B), although high-specification industrial PDV salts are frequently batched or commercially guaranteed at 99.8 to 99.9 percent. Some commercial descriptions and legacy specifications quote different purity thresholds, so the basis of calculation must be checked carefully. A supplier certificate should state the analytical method, result, lot number, moisture basis, and relevant contaminant results instead of relying on a broad claim such as “high purity.”
The following table illustrates the control categories that should appear in a technical specification. Exact numerical limits must be taken from the edition and application standard named in the purchase contract. Where the supplied research does not establish a verified numerical limit, the value should not be inferred from marketing literature.
| Control category | Industrial significance | Verification expected from the supplier |
|---|---|---|
| Sodium chloride assay | Determines the active regenerant concentration and supports repeatable brine preparation | Dry-basis assay, test method, batch result, and stated compliance grade |
| Moisture | Controls flowability, storage stability, caking risk, and feeder accuracy | Measured moisture result, sampling point, method, and specification limit |
| Water-insoluble matter | Indicates the likely burden on screens, sumps, injectors, and resin beds | Insoluble residue result with a defined test method |
| Calcium and magnesium compounds | Can contribute to deposits and reduce the cleanliness of regeneration equipment | Individual or combined impurity results where required by the specification |
| Heavy metals and other trace contaminants | Important for process safety, discharge control, and application-specific compliance | Certificate of analysis with named analytes and limits |
| Physical form | Affects dissolution rate, pneumatic conveying, dust generation, and feeder calibration | Particle-size or tablet-form data, packaging details, and handling guidance |
Compliance certificates also have a practical role in automated production auditing. A certificate of analysis, or COA, allows QA/QC teams to connect a delivery to a silo, a batching record, and a regeneration campaign. That traceability supports validation when conductivity, brine strength, pressure drop, or treated-water hardness moves outside normal control limits. It also helps distinguish a raw-material issue from a mechanical fault, operator error, or resin condition problem.
Trace Insolubles and Their Operational Impact on Ion Exchange Resins
Ion-exchange systems remove dissolved ions by replacing undesirable species with ions held on a functional resin. In sodium-cycle softening, calcium and magnesium are exchanged for sodium, and the resin is later restored with sodium chloride brine. The technology is robust, but it is not indifferent to solids. Particulate matter can settle in brine tanks, collect on underbeds, obstruct strainers, and reach distribution components when filtration or housekeeping is inadequate.
Calcium-magnesium insolubles and other mineral particles create both mechanical and chemical risks. A layer of sediment can reduce the effective volume of a saturator, while deposits on injector nozzles alter flow and produce an incorrect brine dose. Within a resin bed, suspended solids may restrict hydraulic paths and encourage channeling, meaning that part of the bed receives too little contact with the regenerant. Repeated hydraulic stress can also promote resin attrition, fines production, and a gradual loss of usable capacity. The result may be shorter service runs, incomplete regeneration, and premature resin replacement.
Brine chemistry must be evaluated alongside solids control. Sudden changes in acidity or alkalinity can affect material compatibility, contaminant speciation, and the behavior of ionizable functional groups. Because pH is logarithmic, even a one-unit shift represents a tenfold change in hydrogen-ion concentration. The relationship between hydrogen-ion activity and process chemistry is explained in the pH guidance from the US EPA. Brine feed streams must therefore maintain chemical equilibrium, particularly where automated columns depend on repeatable regeneration conditions.
- Inspect saturator sumps and sludge collection points on a defined schedule rather than waiting for low brine strength.
- Check strainers, gravel underbeds, distributor screens, and injector nozzles for restricted flow or visible deposits.
- Trend pressure drop, treated-water hardness, regeneration volume, and brine concentration together.
- Use controlled flushing and approved cleaning procedures to remove accumulated solids without damaging resin or lining materials.
- Investigate changes in salt appearance, dust level, tablet integrity, and insoluble residue after each suspect delivery.
Moisture Dynamics and Anti-Caking Agent Calibration in Bulk Dosing
Moisture is one of the most influential physical variables in bulk salt handling. A low free-moisture specification, often below 0.1 percent where the product and process require it, helps preserve free-flowing behavior. If salt absorbs moisture during storage or transfer, crystals can adhere to one another and form arches across hopper outlets. A silo may appear full while the feeder receives little material, creating apparent dosing failures that are actually flow failures.
Ambient humidity matters, but so do temperature changes, condensation, open access doors, poorly sealed transfer points, and pneumatic lines that carry humid air. Salt can also pick up moisture on cool surfaces after a warm delivery enters a colder plant area. Storage silos should be protected from water ingress, and the air used for conveying should be evaluated for dew point and filtration. Housekeeping is equally important because fines and damp deposits provide nucleation sites for further caking.
Sodium ferrocyanide, known as E535, may be used as an anti-caking agent in some salt products. Regulatory baselines, toxicological limits, and acceptable daily intakes are evaluated in sources such as the EFSA safety evaluation of ferrocyanide anti-caking additives. The allowable concentration is application- and specification-dependent, so the purchasing document must state the permitted treatment and target range in parts per million rather than leaving it to an informal supplier assumption. Operators should not add or adjust E535 at site without a validated formulation, calibrated equipment, and appropriate regulatory review. An anti-caking agent cannot compensate for wet storage, poor silo design, or uncontrolled particle-size segregation.
Feeder calibration should reflect the material actually being handled. Volumetric feeders are sensitive to bulk density, crystal shape, compaction, and moisture. Gravimetric feeders generally provide stronger control because they measure mass directly, but they still require inspection for load-cell drift, buildup, vibration, and bridging. A useful validation exercise is to compare commanded dose, measured mass, and dissolved-brine concentration over several operating cycles. Engineering studies on bulk-solids conveying, slurry hydraulics, and particle suspension dynamics can provide useful frameworks for evaluating dissolution kinetics and flow regimes, though any model must be verified against the facility’s actual geometry, pipe runs, and physical material properties.
Implementing Saturator and Batching Maintenance Protocols
Maintenance should combine physical inspection, instrument verification, and raw-material checks. A saturator is not merely a tank containing salt and water; it is a controlled dissolution system whose performance depends on residence time, contact area, underbed condition, temperature, circulation, and withdrawal rate. The commonly cited saturated brine concentration is approximately 26 percent sodium chloride by mass under suitable conditions, but the measured result depends on temperature and method. “100 percent saturated” should therefore be defined operationally through a validated concentration check, not treated as an assumption.
- Isolate the relevant equipment under the site’s lockout and chemical-safety procedure, then inspect the sump, walls, access covers, level instruments, and overflow arrangements.
- Remove accumulated sludge and fines from the sump and verify that the gravel underbed, screens, and distribution paths are not blinded or displaced.
- Inspect injector nozzles, valves, strainers, and circulation lines for deposits, erosion, or altered flow characteristics.
- Calibrate or verify the refractometer and hydrometer against suitable reference materials at the operating temperature, recording instrument identification and results.
- Sample brine at a defined location and frequency, then compare concentration with feeder mass, water addition, and regeneration demand.
- For silos and hoppers, empty the equipment where safe, remove compacted material, purge transfer lines, clean dust-control components, and inspect discharge gates before refilling.
- Review the delivery COA against the purchase specification, retain a representative sample where required, and release the batch only after QA/QC approval.
Cleaning must avoid introducing uncontrolled water into dry storage equipment. If wet cleaning is necessary, the equipment should be fully drained, dried, and inspected before salt is returned. Pneumatic lines need particular attention because residual moisture can create a hard plug that later breaks loose and contaminates a batch. Dust extraction systems should be checked for differential pressure and filter condition, while all inspection findings should be linked to the delivery lot and maintenance work order.
A preventive checklist should include supplier approval, seal and packaging condition, truck or container cleanliness, lot identification, COA review, moisture result, insoluble-matter result, and confirmation of the supplied physical form. Instrument checks should cover scales, load cells, refractometers, hydrometers, conductivity meters, level sensors, and brine-flow transmitters. Trend data is more valuable than isolated readings: a gradual increase in regeneration volume or a slow decline in brine strength can identify a developing handling problem before it causes hard-water breakthrough or an unplanned shutdown.
Optimise Your Facility with Data-Driven Salt Quality Controls
Strict PDV salt control protects more than chemical purity. It supports stable brine preparation, predictable feeder performance, cleaner saturators, lower solids loading, and more consistent resin regeneration. When moisture and insolubles are measured rather than assumed, maintenance teams can target the actual source of downtime. When every delivery is tied to a COA and a batch record, QA/QC teams can validate process performance and challenge suppliers with objective evidence.
The immediate priority is to compare the current operation with the requirements in the governing specification and the facility’s own process limits. The following actions provide a practical starting point:
- Confirm whether the current salt contract states the correct standard, dry-basis assay, moisture limit, insoluble-matter limit, and anti-caking treatment.
- Audit recent COAs against independent or internal verification results, with particular attention to moisture and insoluble residue.
- Map every point where salt can absorb water, segregate, bridge, or accumulate as fines.
- Recalibrate volumetric and gravimetric feeders using production material, not only a clean laboratory sample.
- Establish brine concentration, treated-water hardness, pressure drop, and resin-capacity trends as linked operating indicators.
- Use the resulting data to set reorder requirements, supplier performance criteria, and preventive-maintenance intervals.
High-purity PDV salt may carry a higher purchase price than an unverified alternative, but the relevant comparison is total operating cost. Avoided injector blockages, reduced sludge removal, fewer emergency cleanouts, longer resin service, and more reliable production often outweigh a modest difference in material cost. For industrial facilities, specification-grade salt is therefore best understood as a process-control input that helps preserve uptime, compliance, and the long-term value of the treatment system.